WITH CONSULTATION!
Industrial Reverse Osmosis Systems
Engineered for deep demineralization, rejecting up to 99% of dissolved salts, silica, and organics for food & beverage, pharmaceutical, and power generation plants.
Submit Inquiry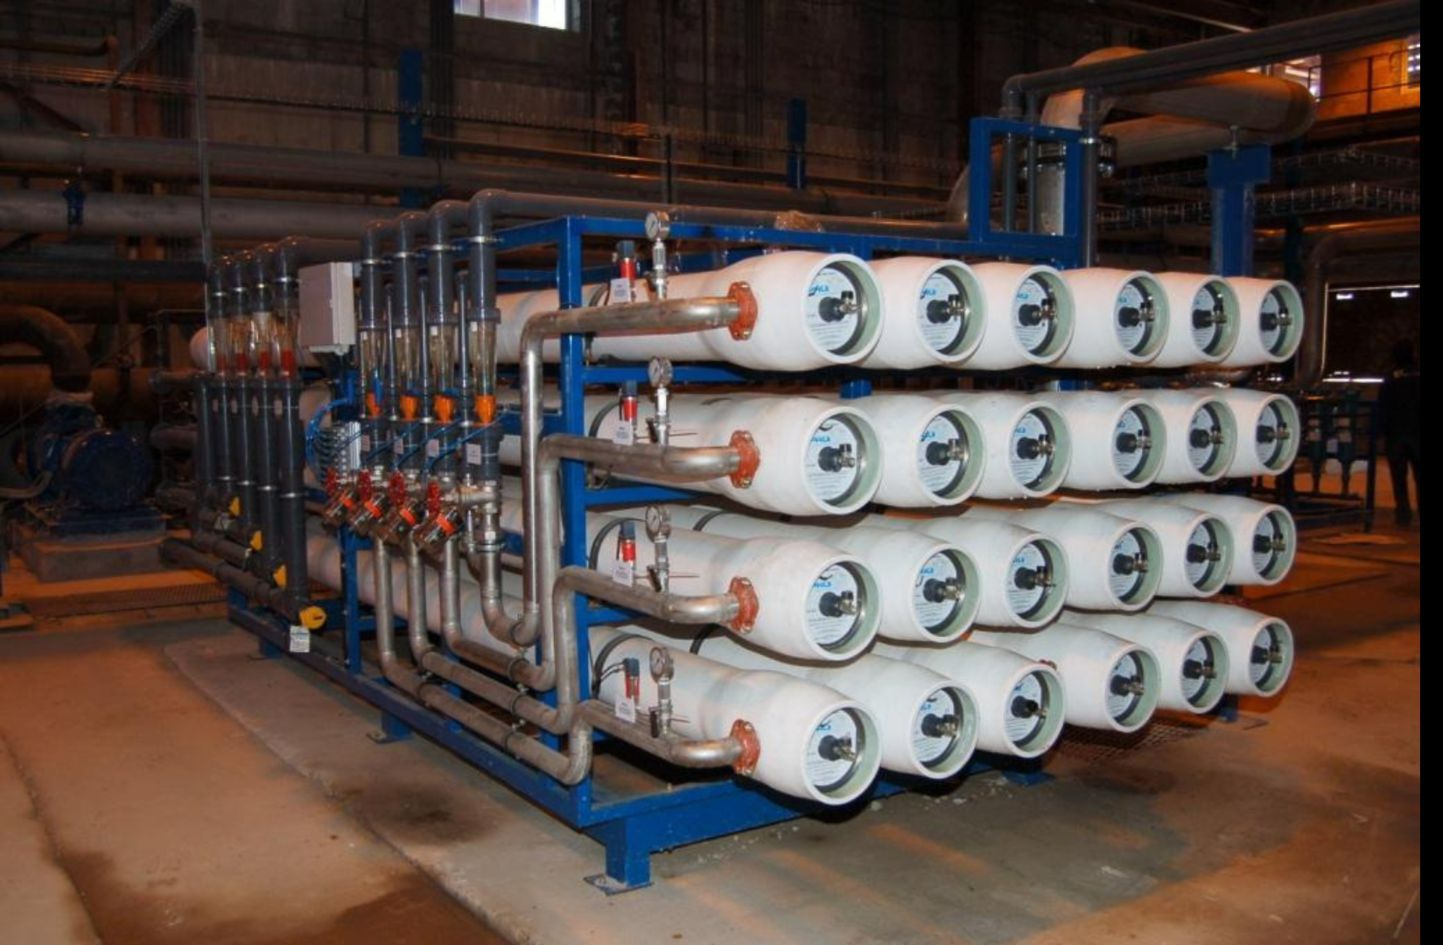
High-purity process water conditioning is critical to manufacturing reliability where water quality directly governs boiler life, product specs, and operational uptime. SUECO industrial reverse osmosis trains achieve up to 99% salt rejection, eliminating heavy metals, silica, and microbiological contaminants across demanding chemical, mining, and food sectors.
Operating Principle of Industrial Reverse Osmosis Systems
The system forces pressurized raw water through 5-micron pre-filtration, whereupon a high-pressure pump drives the stream across semi-permeable spiral-wound reverse osmosis membranes.
The membrane array separates the feed into permeate (purified water) and reject concentrate. Under standard design recoveries, purified water yield ranges between 50–85% of raw feed volume.

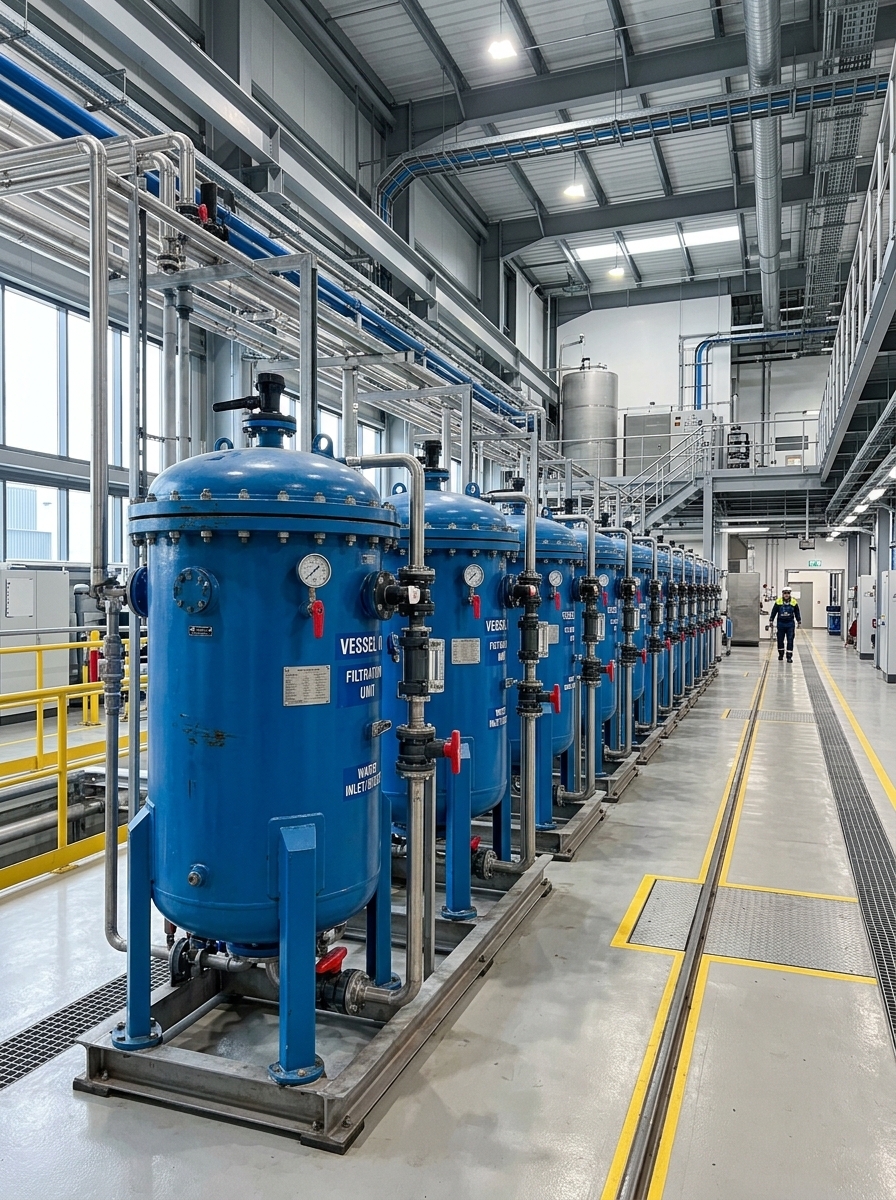
The process train incorporates the following stages:
Primary Sediment Filtration
Removal of silt, suspended particulates, and macroscopic debris.
Coagulation & Flocculation
Agglomeration and precipitation of colloidal organics and fine suspended matter.
Reverse Osmosis (RO)
Membrane demineralization rejecting dissolved solids, heavy metals, and microbes.
Granular Activated Carbon (GAC)
Adsorption of free chlorine, chloramines, trihalomethanes, and dissolved organics.
Ultraviolet (UV) Disinfection
Germicidal UV irradiation destroying bacterial DNA prior to usage or discharge.
Ion Exchange Softening & Demineralization
Cation/anion resin exchange targeting calcium, magnesium, and specific heavy ions.
Strategic Significance
Advanced water treatment engineering is foundational to delivering secure, compliant water supply across municipal, commercial, and industrial sectors. Investing in engineered water conditioning mitigates thermal boiler scaling, protects piping assets against corrosion, curtails lifecycle OPEX, and safeguards natural freshwater reserves.
CONTACT DETAILS
Operating Hours
Mon-Fri: 09:00 – 18:00
Sat-Sun: Closed
Follow Us
Address
Almaty, Bostandyk district, Al-Farabi Ave 7, Block 5A, 13th Floor, Office 203